Introduction of Main Products
A Variety of Available Grades
A total of 9 grades are available: the basic series with 2 grades of hardness, and the alloy series with 4 grades, and the easy welding series with 3 grades, providing a complete product line that can meet a wide range of applications.
Basic Series
This series consists of grades produced with the main emphasis on their hardness levels, the chemical composition being basically simple while the addition of other alloying elements is restrained.
Alloy Series
This series contains alloying elements in greater quantities than the basic series. Both the prescribed hardness and low-temperature toughness are guaranteed.
Easy Welding Series
This series contains restrained contents of carbon and alloying elements. The value of CEV is lower than the standard series and the alloy series, which is good to welding
Grade and Specifications
| Grade | Thickness, mm | Width, mm | Length, mm |
|---|---|---|---|
| B-HARD360A/B (Basic type) | 6-90 | 1300-4200 | 6000-25000 |
| B-HARD360C/D/E (Alloy type) | 6-80 | 1300-4200 | 6000-25000 |
| B-HARD360CFA/B/C/D/E (Easy welding) | 6-20 | 1300-4200 | 6000-25000 |
| B-HARD400A/B (Basic type) | 6-90 | 1300-4200 | 6000-25000 |
| B-HARD400C/D/E (Alloy type) | 6-80 | 1300-4200 | 6000-25000 |
| B-HARD400CFA/B/C/D/E (Easy welding) | 6-20 | 1300-4200 | 6000-25000 |
| B-HARD450A/B/C/D/E (Alloy type) | 6-75 | 1300-4200 | 6000-25000 |
| B-HARD450CFA/B/C/D/E (Easy welding) | 6-20 | 1300-4200 | 6000-25000 |
| B-HARD500A/B/C/D/E (Alloy type) | 6-75 | 1300-4200 | 6000-25000 |
Chemical Composition
| Grade | C | Si | Mn | P | S | Al | Nb | V | Ti | Mo |
|---|---|---|---|---|---|---|---|---|---|---|
| BS600MC, BS600MCK2, BS600MCJ4, BS600MCK4 | 0.12 | 0.5 | 1.9 | 0.02 | 0.01 | 0.015 | 0.09 | 0.2 | 0.22 | 0.5 |
| BS650MC, BS650MCK2, BS650MCJ4, BS650MCK4 | 0.12 | 0.5 | 2 | 0.02 | 0.01 | 0.015 | 0.09 | 0.2 | 0.22 | 0.5 |
| BS700MC, BS700MCK2, BS700MCJ4, BS700MCK4 | 0.12 | 0.5 | 2.1 | 0.025 | 0.01 | 0.015 | 0.09 | 0.2 | 0.22 | 0.5 |
Mechanical Properties
| Grade | Yield Strength MPa | Tensile Strength MPa | Elongation A | Bending Test D - Inner Bending Radius, a - Thickness | Impact Strength Charpy V 20 J |
|---|---|---|---|---|---|
| BS1100 D | ≥1100 | ≥1150 | ≥8 | 90°, D=5a | 40J/-20°C |
| BS1100 E | ≥1100 | ≥1150 | ≥8 | 90°, D=5a | 27J/-40°C |
Wear-Resisting Property
Processing Method
Cutting methods
B-HARD can very well be cut using both cold and thermal cutting methods. The cold methods are abrasive water jet cutting, shearing, sawing or abrasive grinding, while thermal methods are oxy-fuel, plasma and laser cutting.
| Cutting method | Cutting speed | Kerf | HAZ | Dim. tolerance |
|---|---|---|---|---|
| Abrasive water-jet cutting | 8-150 mm / min | 1-3 mm | 0 mm | ± 0.2 mm |
| Laser cutting | 600-2200 mm / min | < 1 mm | 0.4-3 mm | ± 0.2 mm |
| Plasma cutting | 1200-6000 mm / min | 2-4 mm | 2-5 mm | ± 1.0 mm |
| Gas cutting | 150-700 mm / min | 2-5 mm | 4-10 mm | ± 2.0 mm |
Shearing
Note that our setting suggestions are only general recommendations. In practice, the choice is dictated by the machine stability and the condition of the blades.
Blades: The blades should be hard and sharp, with slightly rounded edges.
Clearance: This is the most important parameter for achieving good results. The clearance between the moving and stationary blades should be increased with increasing tensile strength. Incorrect clearance will result in poor sheared surfaces and may give rise to cracking when the plate is subsequently welded or bent.
Rake angle: The larger the rake angle, the lower the shearing force, although the risk will be greater of the plate sliding sideways or the piece of plate that has been sheared off deforming (twisting). As a general rule, the rake angle should be increased when shearing high strength plate.
Shearing force: For a given rake angle, the shearing force increases linearly with increasing strength of the plate.
| Grade | Clearance, Δ in % of t | Rake angle, λ [°] |
|---|---|---|
| B-HARD360 (Basic type) | 13-16 | 2-5 |
| B-HARD360 (Alloy type) | 13-16 | 2-5 |
| B-HARD360CF (Easy welding) | 13-16 | 2-5 |
| B-HARD400 (Basic type) | 13-16 | 2-5 |
| B-HARD400 (Alloy type) | 13-16 | 2-5 |
| B-HARD400CF (Easy welding) | 13-16 | 2-5 |
| B-HARD450 (Alloy type) | 13-16 | 2-5 |
| B-HARD450 (Easy welding) | 13-16 | 2-5 |
| B-HARD500 (Alloy type) | 13-16 | 2-5 |
Oxy-fuel cutting
Preheating
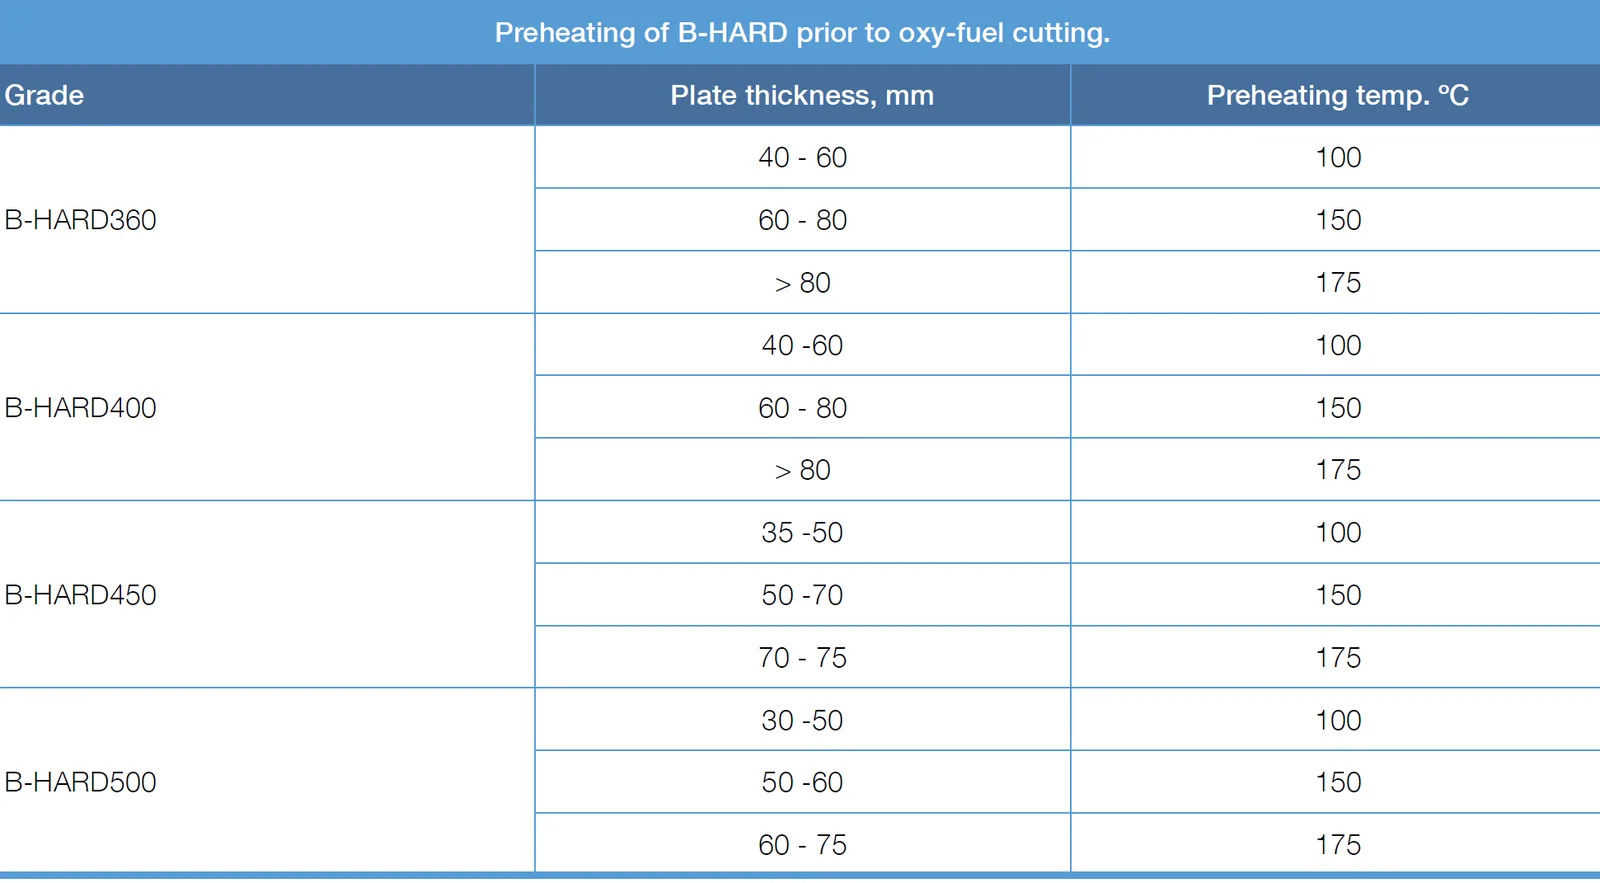
Preheating prior to cutting is the best way of eliminating the risk of cut edge cracking. Preheating is most commonly applied prior to oxy-fuel cutting. The preheating temperature depends on the steel grade and the plate thickness.
| Cutting torch | Thickness (mm) | Cutting speed (mm/min) | Kerf (mm) | Preheat oxygen / Cutting oxygen pressure (Mpa) | LPG pressure (Mpa) |
|---|---|---|---|---|---|
| 0 | 5-10 | 800-900 | 0.8~1.0 | 0.7 | 0.03 |
| 1 | (10)-20 | 700-800 | 1.0~1.8 | 0.7 | 0.03 |
| 2 | (20)-40 | 450-600 | 1.8~3.0 | 0.7 | 0.03 |
| 3 | (40)-60 | 400-450 | 3.0~4.0 | 0.7 | 0.03 |
| 4 | (60)-80 | 340-400 | 4.0~5.0 | 0.7 | 0.035 |
| 5 | (80)-100 | 280-320 | 5.0~6.0 | 0.7 | 0.035 |
Plasma cutting
| Thickness | Current | Vortex ring | PG2 (pressure: bar) | WG (pressure: bar) | Voltage (V) | Cutting speed (mm/min) | |
|---|---|---|---|---|---|---|---|
| Cutting gas (O2) | Compressed air | nitrogen | |||||
| 300A | V4345 | 7.4 | 2.5 | 128 | 5000 | ||
| 10 | 300A | V4345 | 7.4 | 2.5 | 125 | 4100 | |
| 12 | 300A | V4345 | 7.2 | 1.5 | 128 | 3800 | |
| 15 | 300A | V4345 | 7.2 | 1.5 | 132 | 3200 | |
| 20 | 300A | V4345 | 7.2 | 2.5 | 140 | 2000 | |
| 25 | 300A | V4345 | 7.4 | 2.5 | 143 | 1500 | |
| 30 | 300A | V4345 | 6.8 | 2.5 | 145 | 1200 | |
| 40 | 300A | V4345 | 7.2 | 1.5 | 153 | 700 | |
| 50 | 300A | V4345 | 5.7 | 2.2 | 157 | 450 | |
| 60 | 300A | V4345 | 5.7 | 2.2 | 166 | 270 | |
| 75 | 300A | V4345 | 5.7 | 2.2 | 187 | ||
Bending
The bending results are dependent on a number of factors which we have grouped here under three headings: the plate, the tools and the procedure.
| Grade | Thickness, mm | At right angles (R) | At right angles (W) |
|---|---|---|---|
| B-HARD360 | t<8 | R≥2.5t | W≥8.5t |
| t=8-<20 | R≥3t | W≥10t | |
| t≥20 | R≥4.5t | W≥12t | |
| B-HARD400 | t<8 | R≥2.5t | W≥8.5t |
| t=8-<20 | R≥3t | W≥10t | |
| t≥20 | R≥4.5t | W≥12t | |
| B-HARD450 | t<8 | R≥3.5t | W≥10t |
| t=8-<20 | R≥4t | W≥10t | |
| t≥20 | R≥5t | W≥12t | |
| B-HARD500 | t<8 | R≥4t | W≥10t |
| t=8-<20 | R≥5t | W≥12t | |
| t≥20 | R≥7t | W≥16t |
Welding
| Grade | CEV (%) | Welding method | Preheating temp. | Welding consumables |
|---|---|---|---|---|
| B-HARD360 (Basic type, Alloy type, Easy welding) | 0.45-0.58 | GMAW | 6-30mm 100℃ >30-50mm 150℃ >50-90mm 200℃ | 70-100kg |
| B-HARD400 (Basic type, Alloy type, Easy welding) | 0.48-0.60 | GMAW | 6-30mm 100℃ >30-50mm 150℃ >50-90mm 200℃ | 70-100kg |
| B-HARD450 (Alloy type, Easy welding) | 0.55-0.65 | GMAW | 6-30mm 150℃ >30-75mm 200℃ | 70-100kg |
| B-HARD500 (Alloy type) | 0.60-0.70 | GMAW | 6-30mm 180℃ >30-60mm 200℃ | 70-100kg |
| Grade | Thickness (mm) | Diameter of welding stick (mm) | Current (A) | Voltage (V) | Welding speed (mm/s) | Interpass temperature (℃) | Shielding gas | Heat input (kJ/mm) |
|---|---|---|---|---|---|---|---|---|
| B-HARD360 (Basic type, Alloy type, Easy welding) | 6-90 | Φ1.2/1.6 | 150-350 | 20-35 | 5-10 | ≤200 | 80%Ar+20%CO2 | ≤1.5 |
| B-HARD400 (Basic type, Alloy type, Easy welding) | 6-90 | Φ1.2/1.6 | 160-320 | 20-35 | 5-10 | ≤200 | 80%Ar+20%CO2 | ≤1.5 |
| B-HARD450 (Alloy type, Easy welding) | 6-75 | Φ1.2/1.6 | 160-320 | 20-35 | 5-10 | ≤200 | 80%Ar+20%CO2 | ≤1.5 |
| B-HARD500 (Alloy type) | 6-75 | Φ1.2/1.6 | 160-360 | 20-35 | 5-10 | ≤200 | 80%Ar+20%CO2 | ≤1.5 |